
-
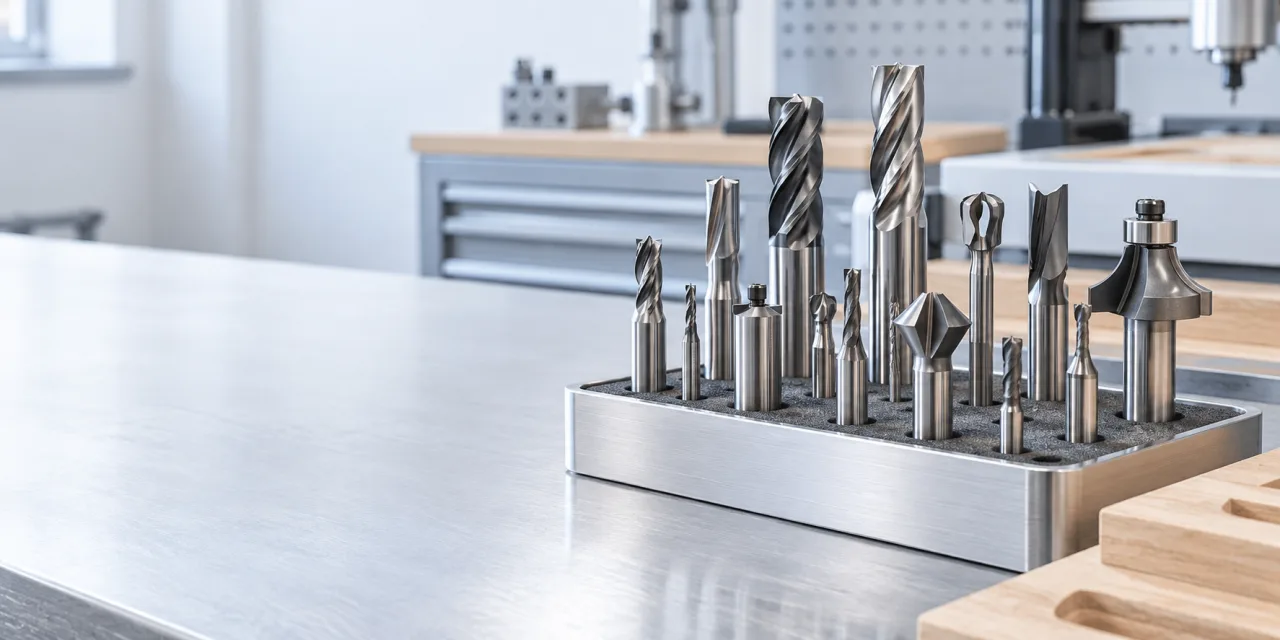
Material grade, condition and stock shape; include coatings or unknown material history.
-
Cutter manufacturer and model, diameter, effective teeth, coating and allowable stickout.
-
Operation
slotting, peripheral roughing, pocketing or finishing; record entry method and CAM strategy.
-
Axial depth of cut and radial engagement, plus toolholder, runout and clamping arrangement.
In this guide
Turn this guide into a buying request
Keep this page as context. Add what you know; review everything before sending. No purchase is made at this step.
Continue to request →Start with the cutting-tool manufacturer’s data for the exact cutter, material and operation, then confirm the machine and workholding can support it. A calculator output is an input to a reviewed setup, not permission to run an arbitrary desktop CNC.
This is a guide to checking specifications and recording a supplier’s test. It does not supply universal cutting settings or replace operator training and the machine’s instructions.
Collect the inputs a meaningful recommendation needs
- Material grade, condition and stock shape; include coatings or unknown material history.
- Cutter manufacturer and model, diameter, effective teeth, coating and allowable stickout.
- Operation: slotting, peripheral roughing, pocketing or finishing; record entry method and CAM strategy.
- Axial depth of cut and radial engagement, plus toolholder, runout and clamping arrangement.
- Machine speed/feed limits and spindle power or torque at the intended speed.
- Approved coolant or dry-cutting arrangement and the guarding, chip control and extraction required.
Two formulas, with units and limits
Table feed in mm/min = spindle speed in revolutions/min × effective cutting teeth × feed per tooth in mm/tooth. In metric units, spindle speed = 1,000 × cutting speed in m/min ÷ (π × effective cutting diameter in mm). Sandvik publishes these relationships.
Feed per tooth is not identical to actual chip thickness in every engagement. Use the tool maker’s treatment of radial engagement, cutter geometry and chip thinning rather than substituting a general internet number.
Illustrative arithmetic, not a cutting recommendation
Assume only for checking the calculation: 12,000 revolutions/min, two effective teeth and 0.02 mm/tooth. Table feed is 12,000 × 2 × 0.02 = 480 mm/min. These invented inputs are not approved settings for aluminium, wood or any machine.
Reducing spindle speed to 9,000 at the same nominal feed per tooth gives 360 mm/min. Keeping 480 mm/min instead changes nominal feed per tooth to about 0.0267 mm/tooth. This is why an RPM change and a feed change should be reviewed together.
Public-manual check: travel speed is not an approved cutting feed
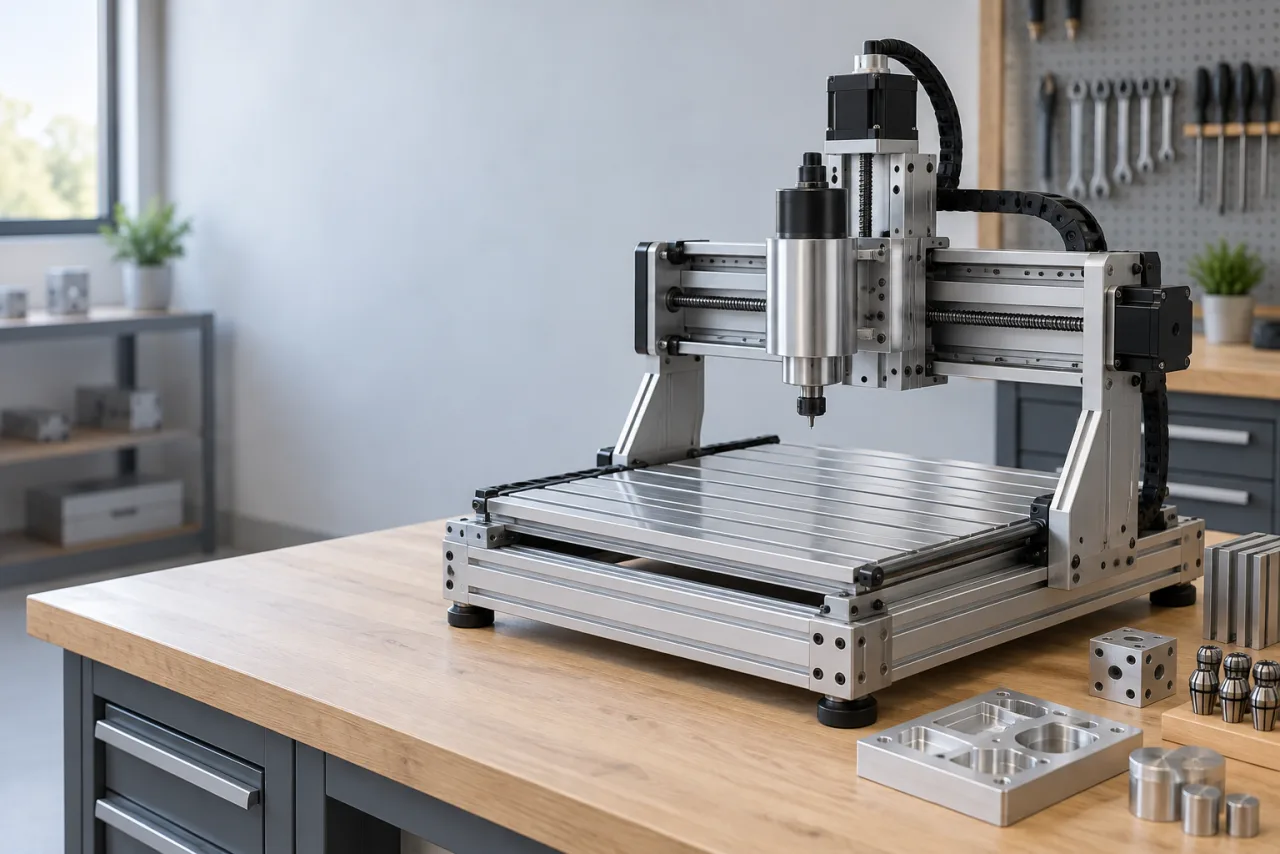
We read the manufacturer-linked Genmitsu 3030-PROVer MAX manual, cover revision V1.0 Jun 2023, on 2 October 2026. Printed page 03 lists a 300 × 300 × 78 mm work area, a 300 W spindle and a 2,000 mm/min maximum speed. None of those entries identifies a tool, aluminium alloy, engagement or measured part result.
The buyer’s conclusion is limited: those figures help screen a proposed setup for obvious mismatches, but cannot approve a cutting feed. Ask for the offered machine revision and its own instructions. A current Ultra variant or an upgraded spindle must not inherit the older MAX manual’s limits without confirmation.
Reject a demonstration that cannot be tied to the offered configuration
- If the seller shows an aluminium test but omits the alloy, tool model or depth/engagement, request the missing record before using it to compare machines.
- If only one easy surface is measured, identify the tightest required feature and how it will be checked. A photograph of a pocket is not a dimensional report.
- If a stronger spindle, different controller or fixture was used, price and validate that actual configuration. Do not call an upgraded demonstration evidence for a lower-cost base kit.
- If the stated program/feed does not match the recorded run, mark the comparison unresolved. Ask for one controlled repeat with a saved revision rather than a sequence of undocumented adjustments.
Do not apply one fix to every broken cutter
Tool breakage can involve overload, runout, poor holding, collision, chip recutting, unsuitable geometry, wear or material variation. A sound or chip shape alone cannot diagnose the cause. Stop the operation safely and have the setup reviewed before continuing; do not reach into moving machinery to inspect chips.
A controlled test record the buyer can review
- Before: approved program, work offset, stock size, tool details, fixture and safety checks.
- During: actual spindle speed and feed, axial and radial engagement, cooling method, interruptions and alarms.
- After: measured features and units, surface observations, tool wear, cycle time and any rejected result.
- Changes: what was changed, why, who approved it and which subsequent part was measured. Avoid changing several variables without recording them.
- Decision: passes the stated part requirement, needs another test, or is unsuitable. Never turn one short demonstration into a general production guarantee.
Keep safe operating instructions model-specific
For example, Haas instructs users of its mills to operate with functioning door interlocks and to restrict electrical-panel access to qualified personnel. Apply the purchased machine’s own instructions and local requirements; this example is not a retrofit recipe for another machine.
Use the evidence to buy the right machine
Send a proposed tool and material specification with the RFQ. Ask the seller to justify test conditions from its machine and tool documentation. If it cannot make the required part without an unsupported workaround, reconsider the machine instead of assuming different feed settings will cure it.
Use a repeatable supplier test brief
The blank brief separates the part requirement, proposed setup, evidence returned and buyer disposition. It deliberately contains no recommended cutting settings or invented test result. Send it with the proposed part so candidates can explain what they can demonstrate and what remains unverified.
Download the CNC purchase and test-evidence brief (plain text) ↗
What to ask the seller
Get details for the exact item before approving a purchase.
- What model and revision is being shipped?
- Can the seller provide photos of the actual item and its condition?
- What accessories and documents are included?
- What are its packed dimensions and weight?
Plan the CNC inspection
Ask for a photo checklist of the goods received before international shipping.
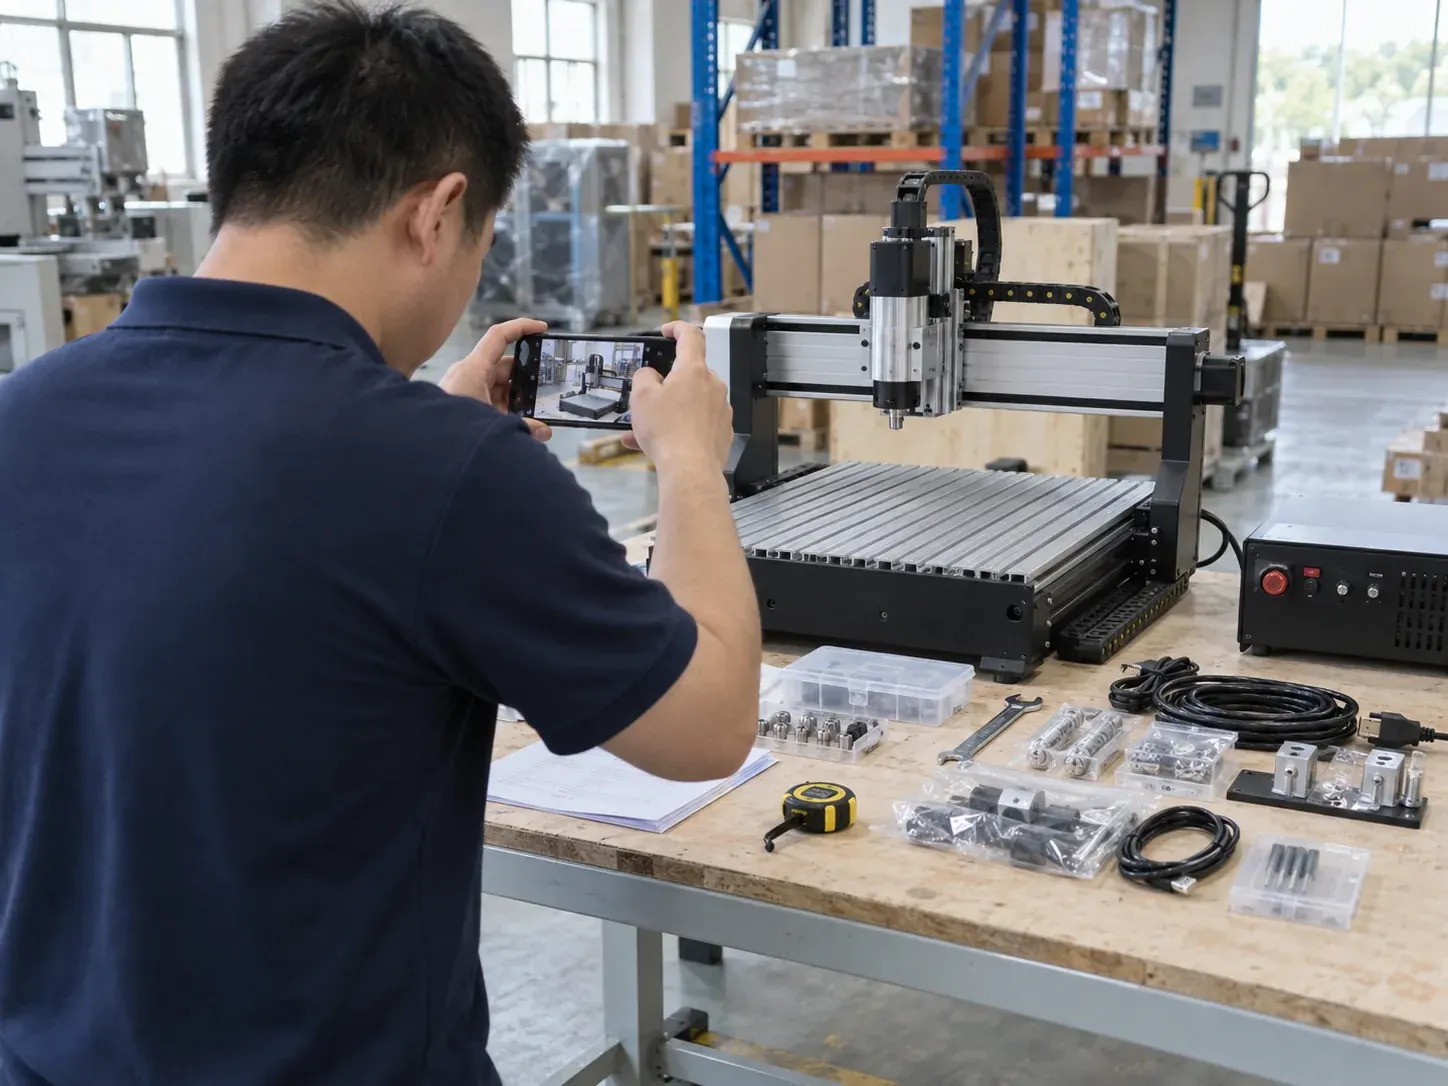
- Item, model and quantity
- Visible condition and included accessories
- Packaging before dispatch
Common questions
- Should I simply reduce depth and keep the feed?
- Not as a universal rule. Review radial engagement, tool geometry, spindle speed, workholding and the manufacturer’s recommended conditions together.
- Does aluminium always need a mist system?
- No universal coolant prescription applies. Follow the cutter and machine instructions and the fluid safety information. Include any required containment, extraction and maintenance.
- Can I judge a safe cut by sound?
- Sound may help a trained operator identify a change, but cannot establish safe conditions or prove dimensional acceptance. Use a reviewed setup and measurements.
 Desktop CNC machines for metal: prove the job before buying
 Buying your first CNC router: a practical checklist