
Explain Reserved Empty ATC Pockets in the CNC Tooling Handover
An empty magazine position can be a deliberate reservation. Reconcile the approved tooling plan, ordered assemblies and provider-declared pocket status before calling it a shortage.
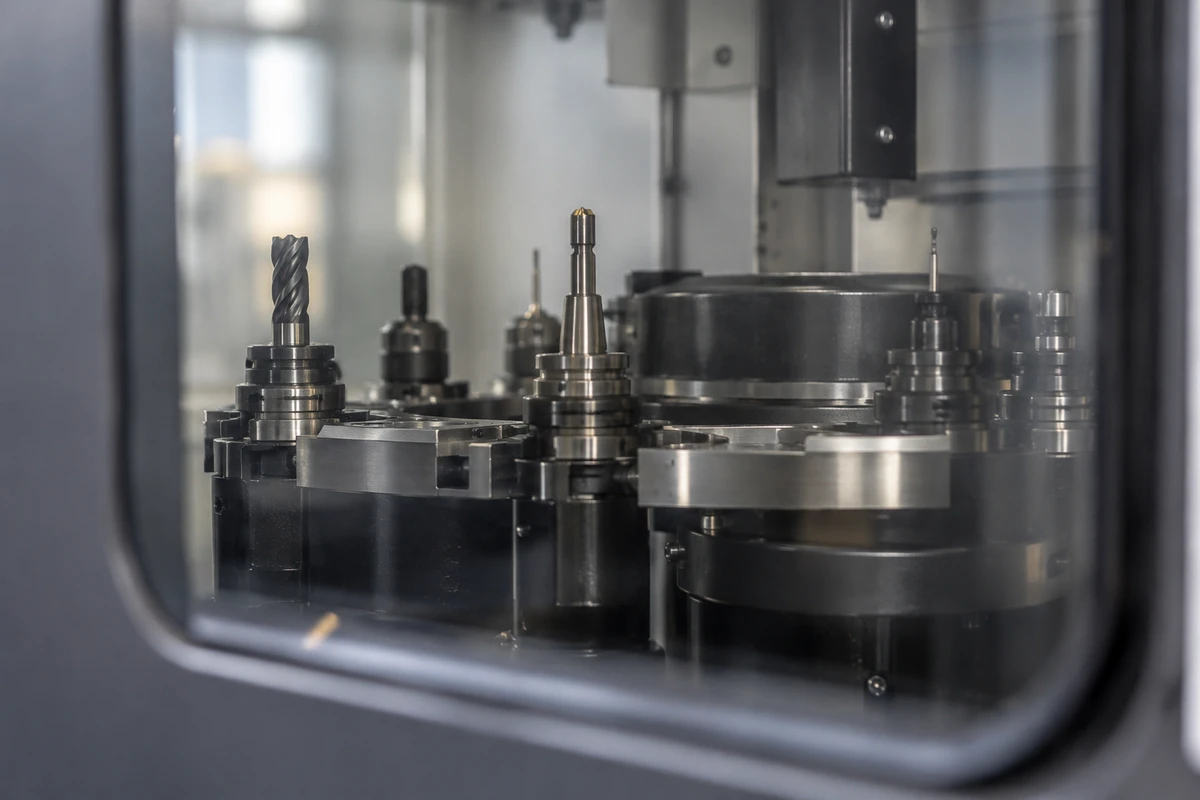
Empty magazine positions do not automatically mean that purchased holders are missing or that extra tools can be added. A CNC ATC reserved pocket handover should explain which apparent vacancies are deliberate reservations under the qualified provider’s approved tooling plan.
Begin with the machine/changer configuration and approved tool assemblies already established. The buyer’s decision is whether the delivery records reconcile the empty positions with that plan and the purchased supply. This article does not choose holders, design a loading arrangement, edit a tool table or authorize anyone to occupy a pocket.
Keep three documentary counts distinct
Record the machine’s nominal magazine-position count, the count of purchased assemblies actually delivered and the provider-approved occupancy for the identified plan. They describe different things. An order may include a defined tooling set without buying one assembly for every nominal position.
Ask the supplier to state what the purchase agreement actually promises. A machine specification naming a magazine count is not the same as an invoice listing included holders and cutters. Conversely, an explicitly missing ordered assembly remains a delivery question even if the tooling plan also includes deliberate reservations.
Keep these questions separate in the reconciliation. Do not use a reservation explanation to dismiss an actual shortage, and do not buy additional tooling merely to make a photograph resemble a full magazine.
A location reference is not an availability statement
The handover may already identify each physical assembly, its controller identifier and its captured pocket location. That mapping answers where the provider says an assembly is represented in the recorded state. It does not establish whether an adjacent empty position is available.
Ask for the qualified provider’s reservation explanation and the approved loading or clearance-plan reference. Each disputed vacancy should have an attributable status for the stated plan: deliberately reserved, unassigned as declared by the provider, or unresolved. These are documentary categories for review, not instructions for the reader to arrange tools.
Keep the captured state and plan revision visible. A record for an earlier assembly set cannot silently establish the status of the present set. Likewise, a provider-declared unassigned or available status belongs only to the identified plan and state; it is not a new loading authorization.
Preserve manufacturer classifications and their limits
The cited Haas Mill Operator Manual distinguishes large and heavy designations and describes adjacent-empty-pocket requirements for large tools. It also has an XL option with a taper-specific qualification. The documented arrangement permits shared adjacent empty positions. These are features of that Haas implementation, not flags or rules that every ATC uses. Haas Mill Operator Manual, Tools – Tool Table
Ask the provider to identify the actual classifications and applicable manufacturer basis for the supplied machine. Preserve large, heavy and XL as distinct source terms where relevant rather than translating them all into one generic “oversize” category.
A heavy designation does not answer the same documentary question as a large-tool reservation. Nor does a broad tool description establish which rule applies to a complete cutter/holder assembly. The qualified integration owner must supply the plan-specific explanation; procurement should not classify the assemblies from appearance.
Do not calculate available capacity by a generic subtraction
An attractive shortcut is to start with nominal pocket count and subtract a fixed allowance for every large tool. That would assume a pattern the actual provider has not established. The Haas example’s shared-empty-position qualification is one reason such a universal formula is inappropriate.
Instead, request the provider’s approved occupancy statement for the exact assembly set and its referenced plan. Keep purchased quantity, deliberate reservations and unresolved positions visible without deriving a new arrangement. A count can summarize the provider’s declaration; it should not create it.
If the seller’s proposal advertises additional usable capacity, ask which plan and assemblies support that claim and who has reviewed it. Record a proposed change separately from the already approved delivery. The buyer’s desire to use more tools does not extend the current plan’s authority.
Resolve a fictional missing-holder claim
Imagine a fictional buyer sees empty positions in a supplied machine record and reports missing holders. The order reconciliation shows that every purchased assembly was delivered. The qualified provider’s plan identifies deliberate reservations associated with the documented large-tool requirement.
The buyer asks the provider to connect that explanation to the current approved assembly set and the disputed positions. It then keeps the purchased-quantity conclusion separate from the reservation status. It does not move tools, clear classifications or order extra holders to fill the visual gaps.
Suppose one empty position is absent from the provider’s explanation. That position remains unresolved. The supported reservations do not justify classifying every other vacancy the same way. Ask for the missing plan-specific status rather than assuming either a shortage or usable capacity.
Alternatively, the paperwork may reveal that an ordered assembly really is missing. Keep that shortage open under the supplier’s delivery response while preserving the valid reservation explanation. The reconciliation should allow both findings to exist without forcing every empty position into one category.
Reopen the plan when an assembly changes
A proposed cutter or holder change should return to the qualified integration owner for its effect on the approved tooling plan. Even if the purchase description looks similar, the buyer should not assume the prior reservation explanation covers the new complete assembly.
Ask the provider to identify the changed set revision and the affected handover records. Retain the old plan as historical evidence and the new proposal with its actual approval status. A corrected packing list alone does not approve changed occupancy.
Close this document requirement when the purchased assemblies are accounted for and the provider has explained reservation status for the relevant plan and captured state, with gaps explicit. That closure is a delivery-record conclusion. It supplies neither a tool-loading instruction nor a tool-change safety or performance approval.
Buyer document-review worksheet
This original worksheet organizes the provider’s evidence. It is not a manufacturer form or a technical work instruction. Keep the original source reference beside each answer.
| Field | Answer to obtain |
|---|---|
| Machine/changer configuration | Exact changer implementation and relevant machine variant |
| Approved assembly set revision | Approved complete assemblies and controlled set issue |
| Nominal position count | Manufacturer or supplier specification, at its actual scope |
| Delivered purchased assembly count | Order lines reconciled with delivered assemblies |
| Provider reservation explanation | Plan-specific explanation and applicable source basis |
| Approved plan reference | Qualified plan issue associated with the supplied set |
| Provider-declared reserved, unassigned or unresolved status for the identified plan/state; no inferred usable capacity | Provider-attributed status for the captured state only |
| Qualified change-review owner | Named authorized integration owner and change-review route |
Bring the precise gap into the inquiry
For broader product context, see CNC router spindles. As an independent buying agent, we can coordinate supplier questions within an agreed purchasing scope. Specialist work, its availability and its approval require the responsible qualified provider.
Start a CNC quote request with a supported listing link, description or permitted product images. Arrange manuals, drawings, data files and service records through a separately authorized exchange; the form’s image field is not a technical-file upload channel.
Frequently asked questions
Does an empty ATC pocket mean a holder is missing?
Not necessarily. Compare the purchased assembly list with delivery evidence and ask the qualified provider whether the vacancy is reserved, unassigned or unresolved under the identified plan. A real ordered-item shortage remains a separate issue.
Are large and heavy tool designations interchangeable?
Do not merge them. The cited Haas implementation distinguishes the concepts, and the actual provider must explain their applicability to the approved assembly set and machine configuration.
Can usable capacity be calculated by subtracting a fixed number for each large tool?
This article supplies no such formula. Obtain the qualified provider’s occupancy statement for the actual plan; the documented example allows shared adjacent empty positions, so a generic subtraction could misrepresent the arrangement.
Can a provider-declared unassigned pocket be filled with a new tool?
The handover status describes a specific approved plan and captured state. A new assembly or changed arrangement needs the qualified integration owner’s review; the documentary label is not loading permission.
Sources
Discuss a sourcing request related to this article.Explain Reserved Empty ATC Pockets in the CNC Tooling Handover